Steel fabrication · Shandong, China

Steel fabrication and precision metal parts, built to drawing

// Since — 2004 //

Structural steelwork, laser cut plate, formed sheet and machined parts, fabricated from your drawing.
Execution
EN 1090-2 EXC2
Machining
±0.02 mm · IT7
Plate
0.5–25 mm laser
Modules
to 12 m shipped
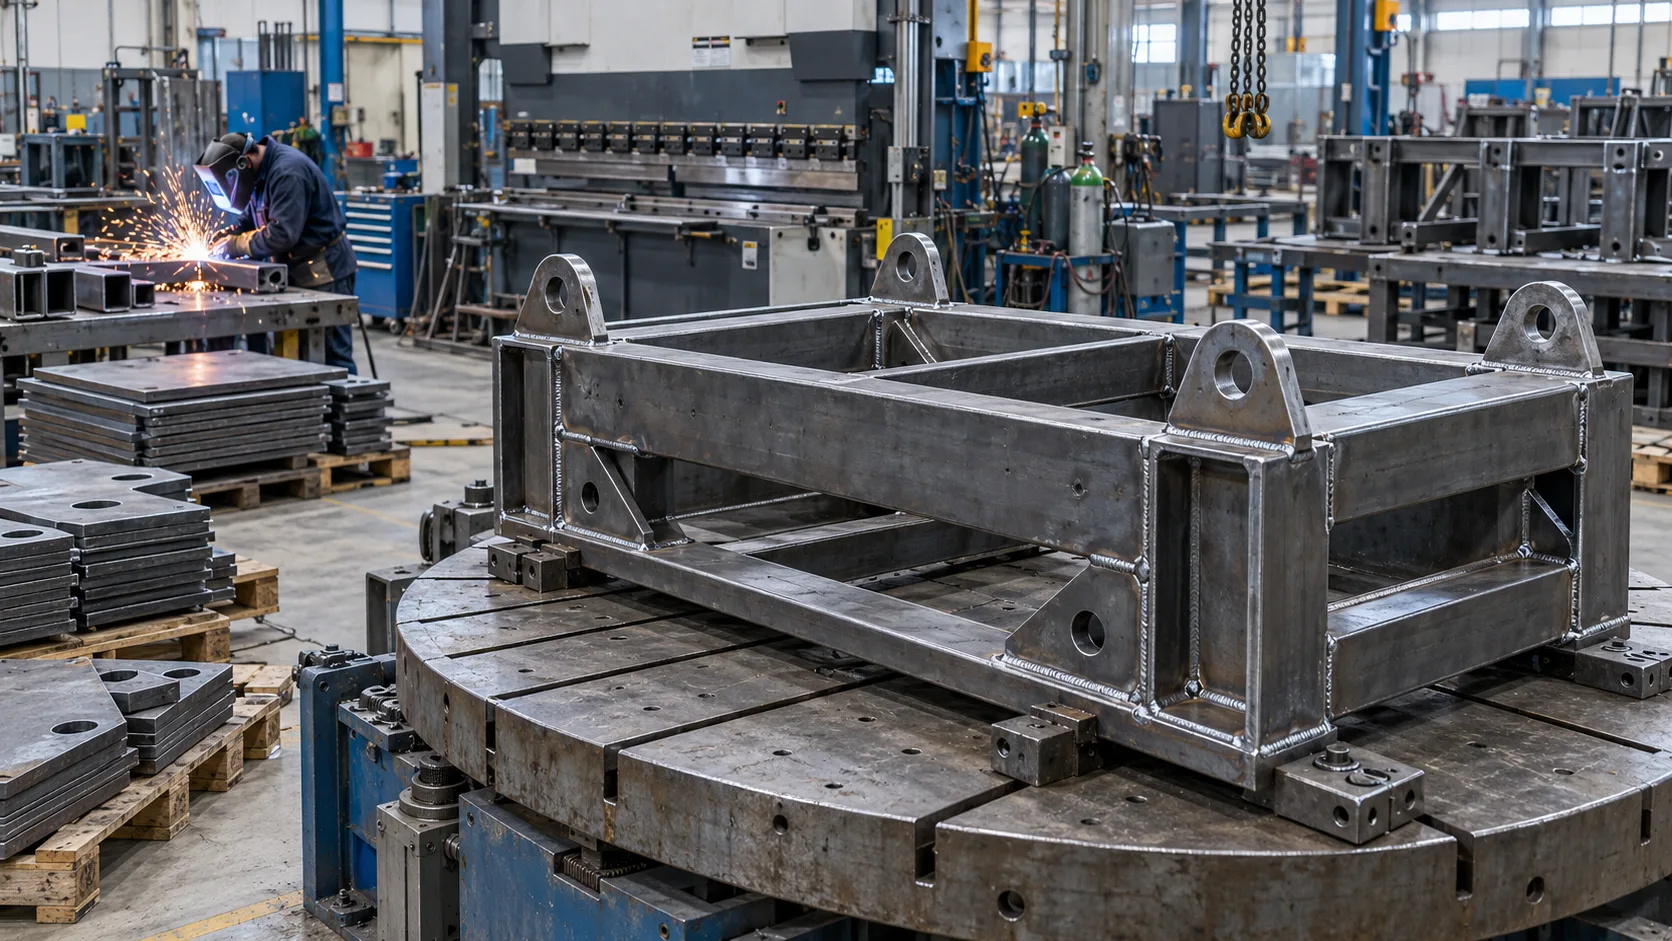
Freshly welded steel assemblies on a turning table in a fabrication bay, with stacked plate and a welder's sparks behind

Fabrication lines

Five fabrication lines

Five routes in one shop, each inspected against the tolerance band on your drawing.

Welded steelwork — BM-S355 produced by Brantmoor, photographed on a cool grey-blue seamless backdrop

BM-S355

Welded steelwork

  • EN 1090-2 EXC2 · S355JR
  • ISO 3834-2 welding
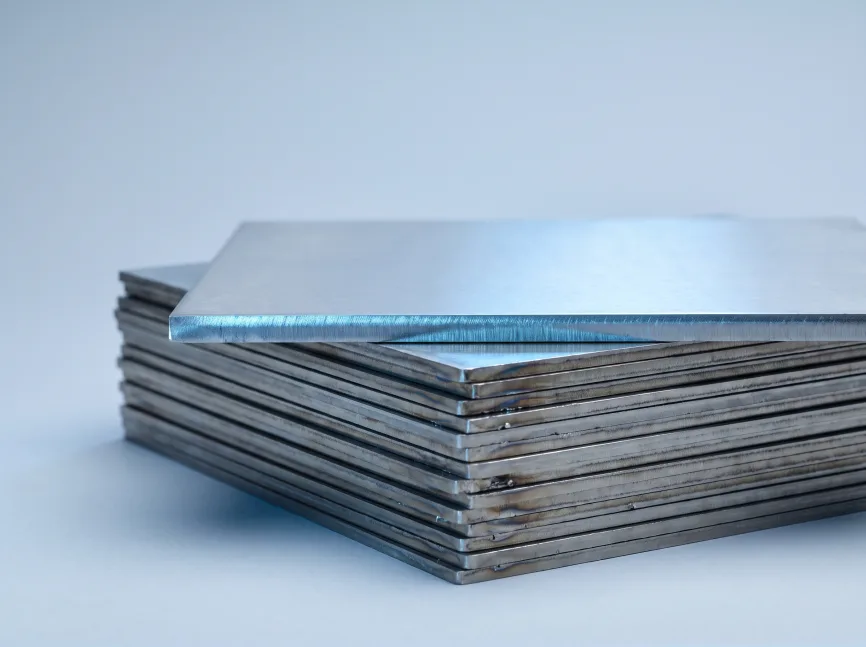
Laser cut plate — BM-LASER produced by Brantmoor, photographed on a cool grey-blue seamless backdrop

BM-LASER

Laser cut plate

  • 0.5–25 mm · ±0.10 mm
  • Q235B / 304 / 6061-T6
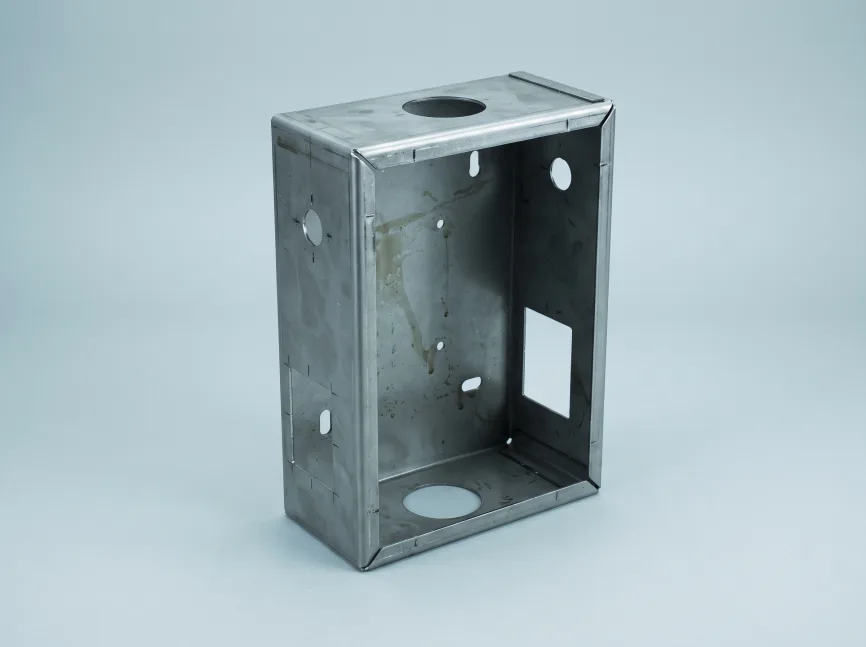
Press-braked parts — BM-PRESS produced by Brantmoor, photographed on a cool grey-blue seamless backdrop

BM-PRESS

Press-braked parts

  • 400 t · 4 000 mm
  • ±0.5° bend angle
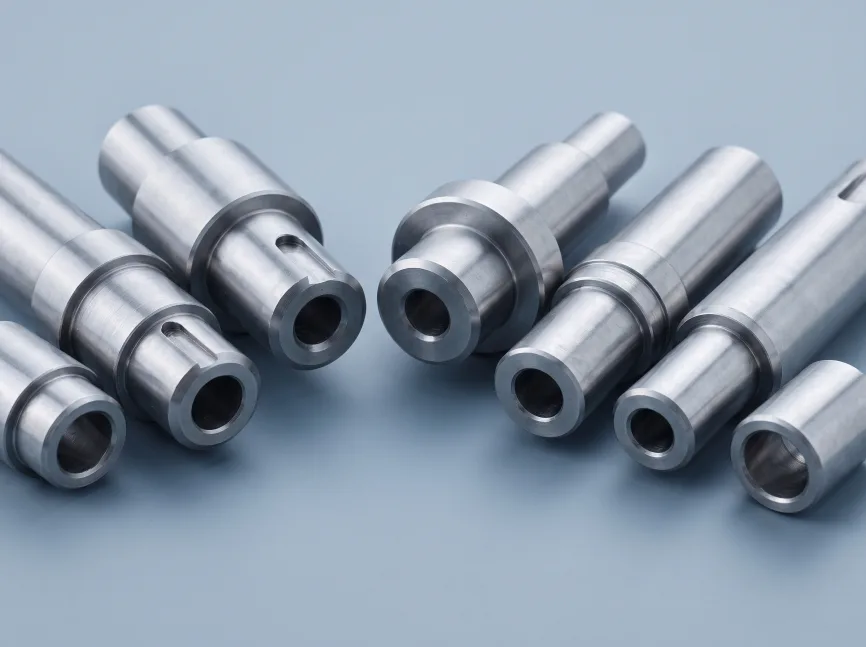
Machined components — BM-CNC produced by Brantmoor, photographed on a cool grey-blue seamless backdrop

BM-CNC

Machined components

  • ±0.02 mm · IT7
  • Ø520 × 1 000 mm turned
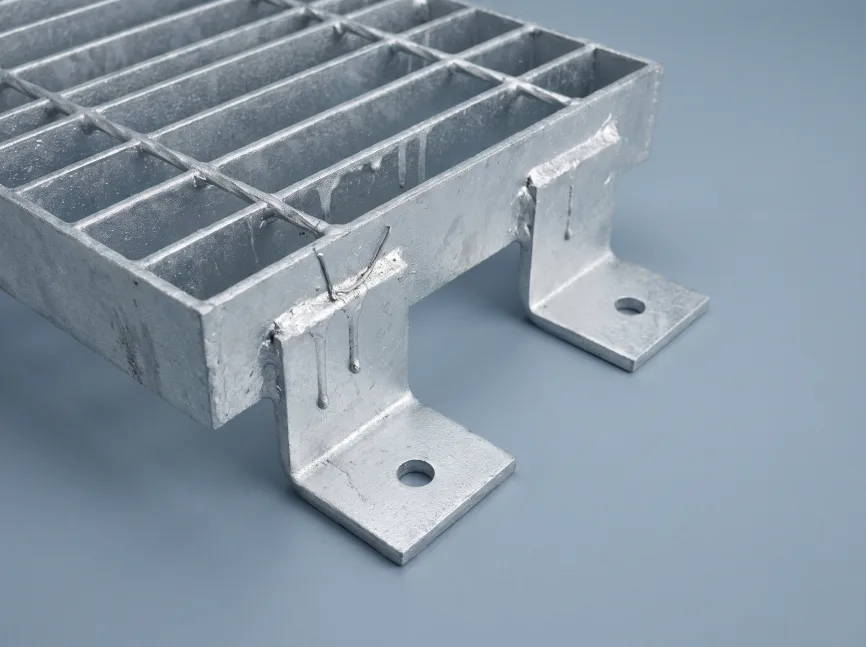
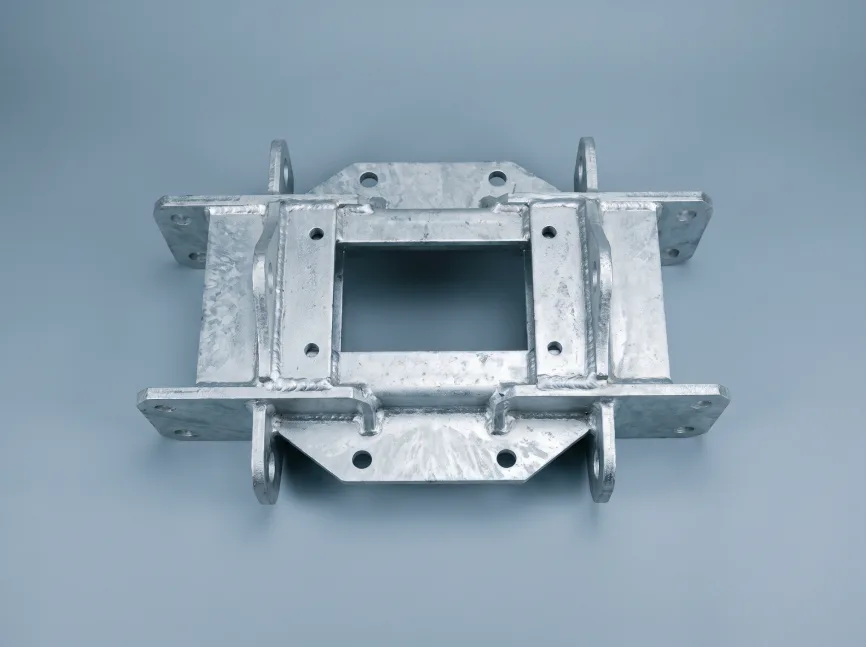
Hot-dip galvanizing — BM-HDG produced by Brantmoor, photographed on a cool grey-blue seamless backdrop

BM-HDG

Hot-dip galvanizing

  • ISO 1461 · 85 µm min
  • ASTM B117 · 480 h

Route card

One part, six steps

Six gates, same order every job. Your drawing decides which one matters most.
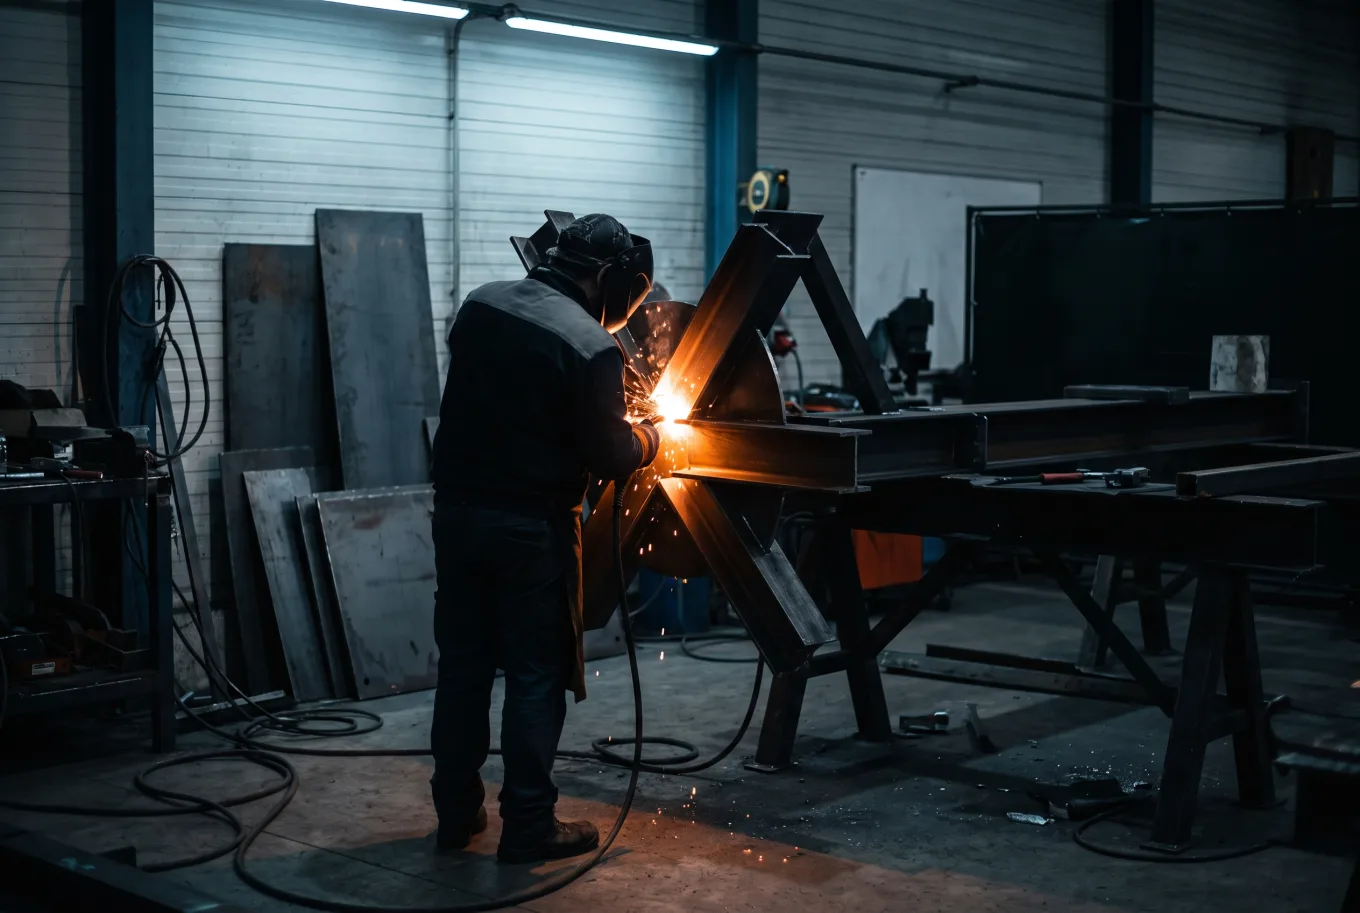
A welding station building a structural steel node on the shop floor, the arc the brightest point in the frame

01

Drawing and WPS review

DXF, STEP or PDF in. We confirm the material grade, the tolerance band and the EN 1090-2 execution class before quoting.

02

Cutting

Fibre laser 0.5–25 mm to ±0.10 mm on profile; plasma to 60 mm for thicker plate.
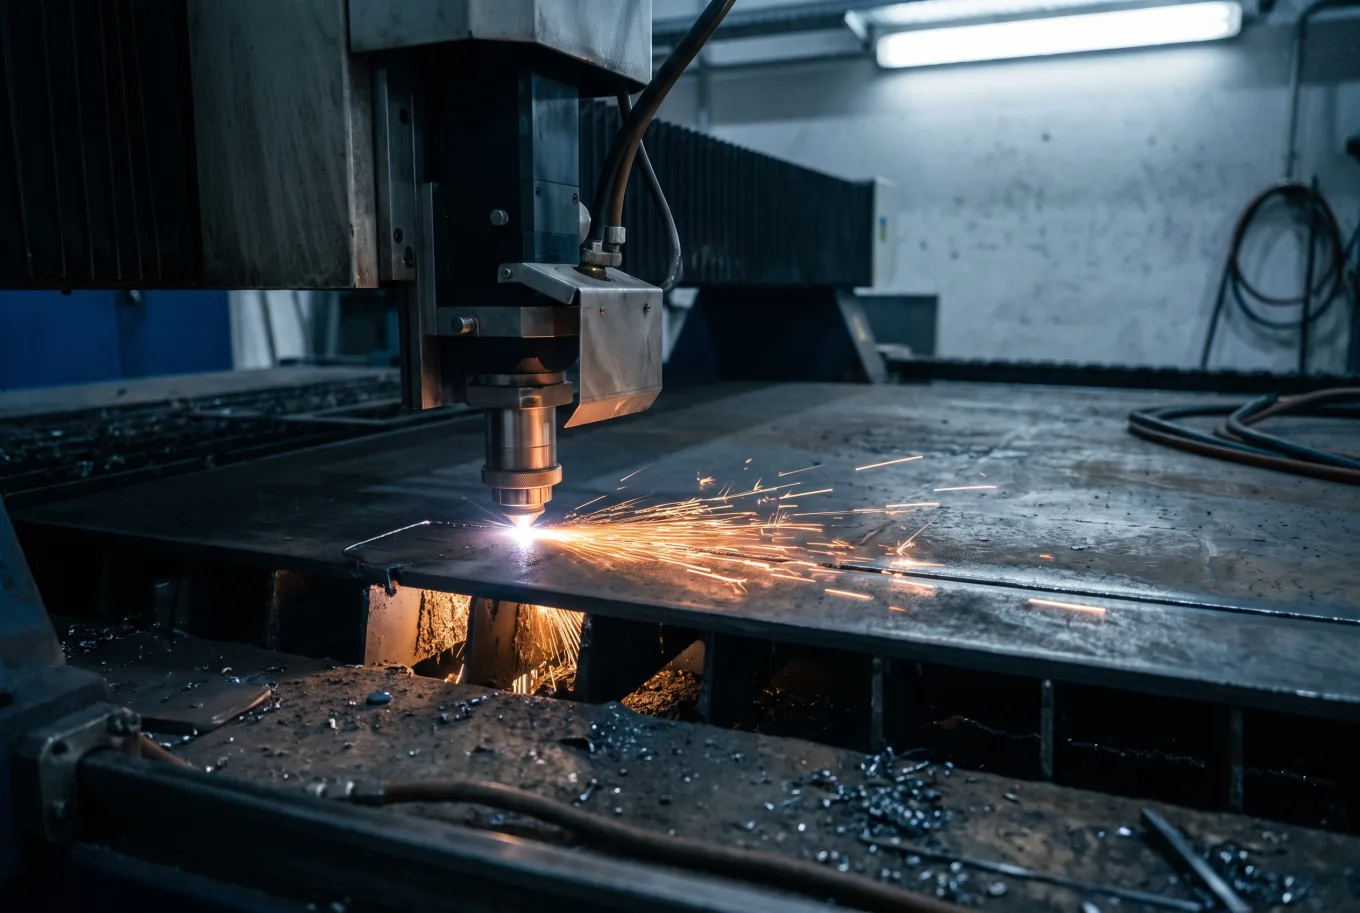
Cutting at Brantmoor — Fibre laser 0.5–25 mm to ±0.10 mm on profile; plasma to 60 mm for thicker plate.

03

Forming

400 t press brake on a 4 000 mm bed, ±0.5° bend angle; plate rolled to Ø800 mm.
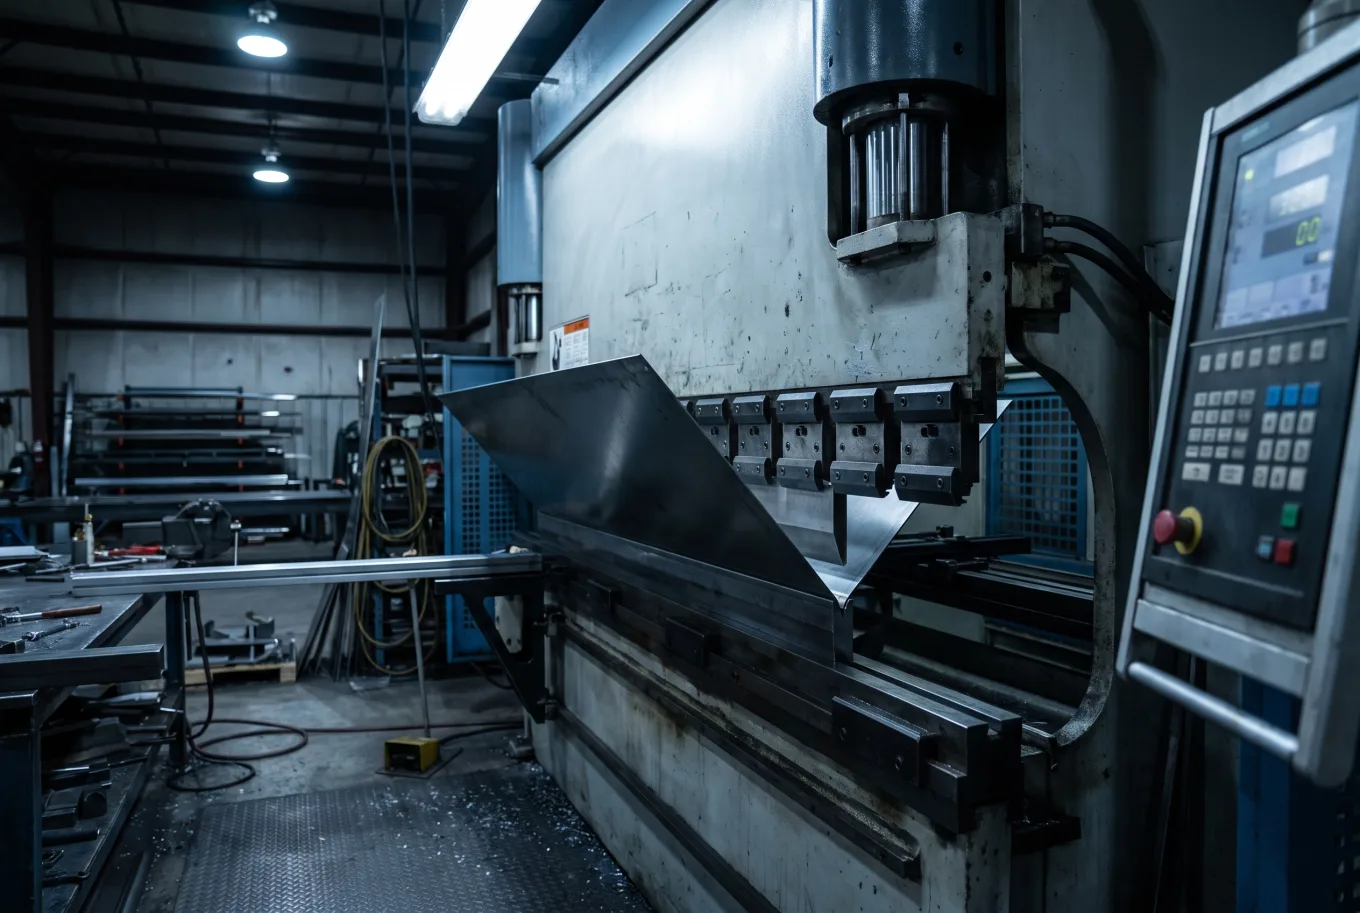
Forming at Brantmoor — 400 t press brake on a 4 000 mm bed, ±0.5° bend angle; plate rolled to Ø800 mm.

04

Welding

WPS qualified to EN ISO 15614-1, welders coded to EN ISO 9606-1 and AWS D1.1.

Welding at Brantmoor — WPS qualified to EN ISO 15614-1, welders coded to EN ISO 9606-1 and AWS D1.1.

05

Machining

CNC turning and 3/4-axis milling to ±0.02 mm, IT7 roundness, Ra 0.8 µm.
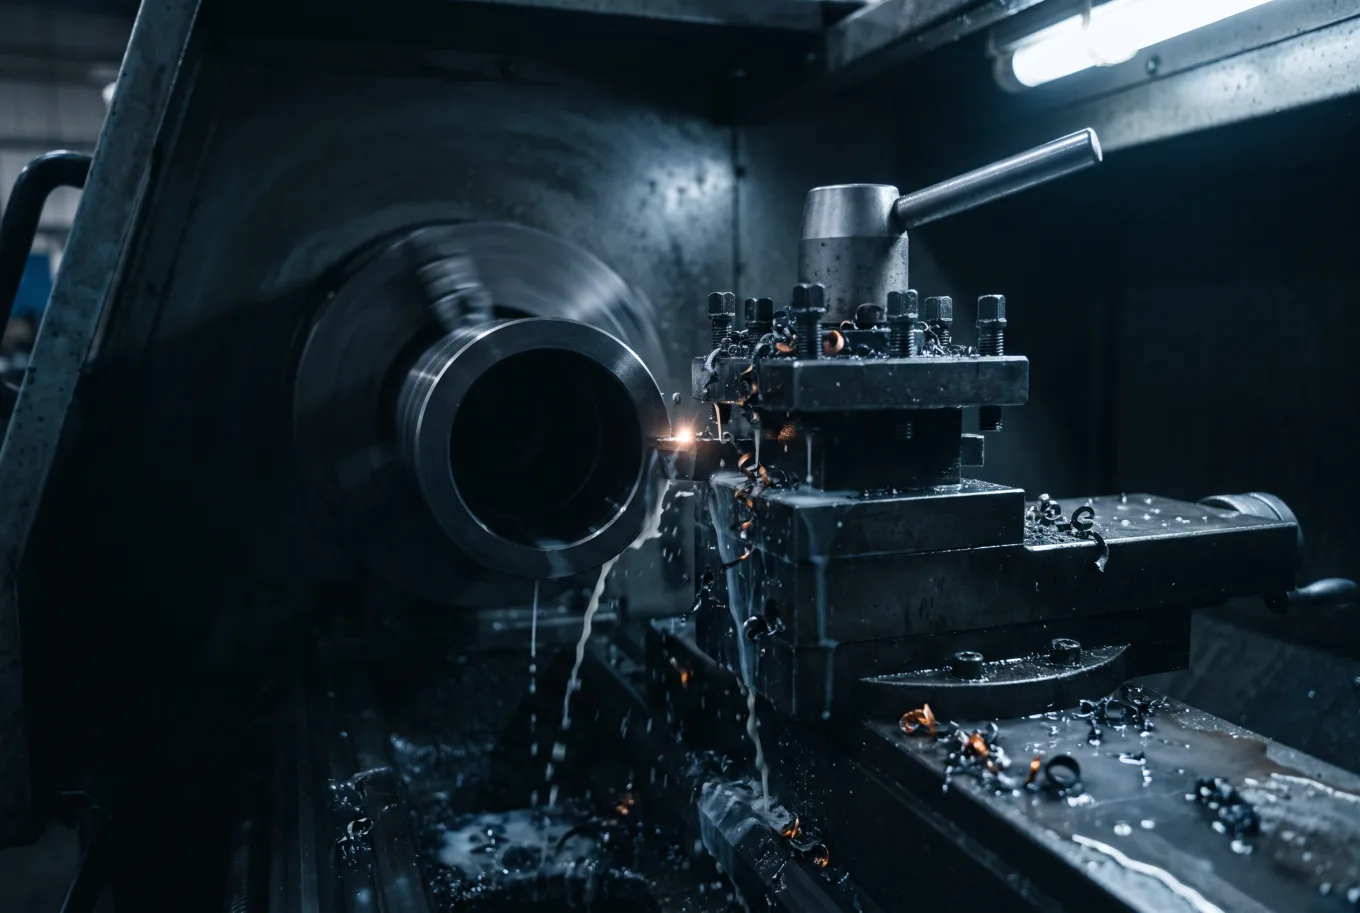
Machining at Brantmoor — CNC turning and 3/4-axis milling to ±0.02 mm, IT7 roundness, Ra 0.8 µm.

06

Inspection and finishing

Dimensional report, 100% visual and 10% MT, then ISO 1461 galvanizing or ISO 12944 coating.
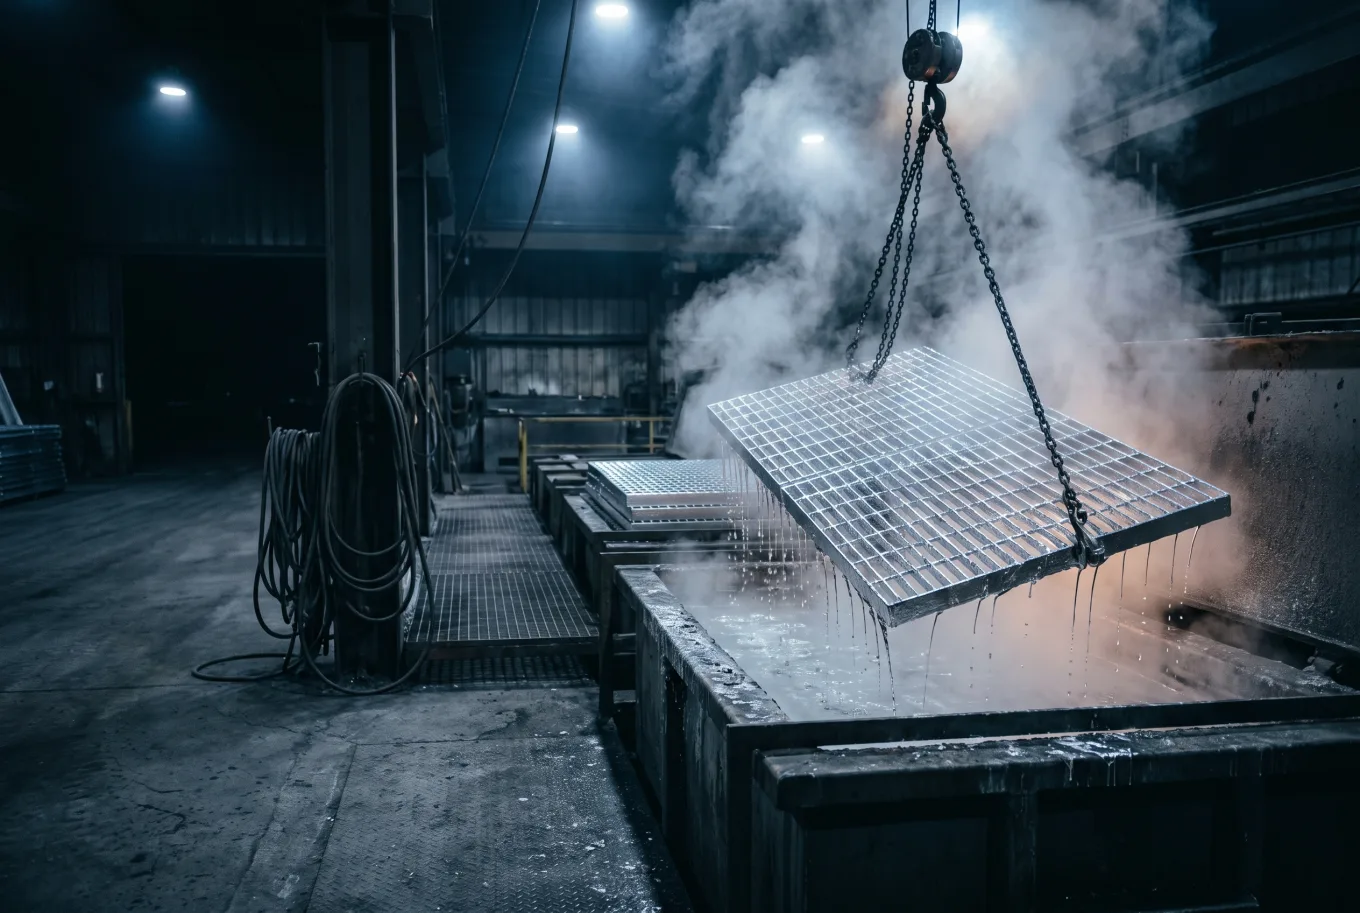
Inspection and finishing at Brantmoor — Dimensional report, 100% visual and 10% MT, then ISO 1461 galvanizing or ISO 12944 coating.

Applications

Where the parts go

Three working conditions, and the one number on each that decides the part.

Industrial steelwork

BM-S355 · BM-HDG

Decided by
Execution class and corrosion system

EXC2 is the default for portal frames and conveyor supports; coastal and agricultural work goes out galvanized to ISO 1461 rather than painted.

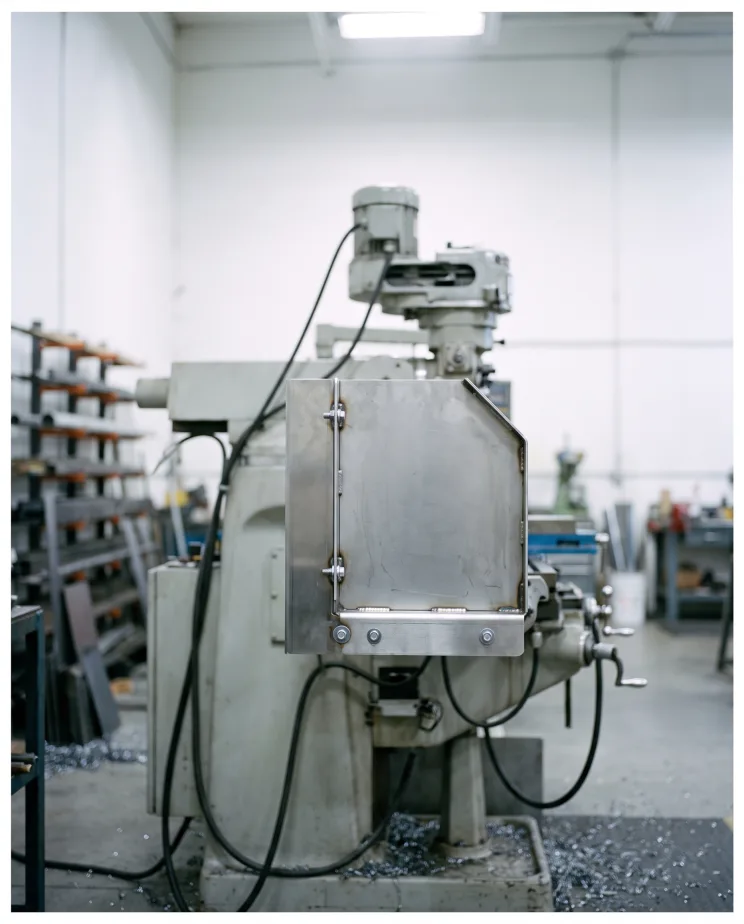
Machine guards and enclosures

BM-LASER · BM-PRESS

Decided by
General tolerance against the drawing

ISO 2768-1 class m covers most guards and covers. Where a bearing or a seal seats, the drawing calls out the tighter band and the part moves to machining.

Outdoor and coastal parts

BM-HDG · BM-CNC

Decided by
Coating life in the service environment

ISO 12944 C3 to C5 decides the system, not the colour. Cut edges and threads are the first place a coating fails, so they are specified separately.
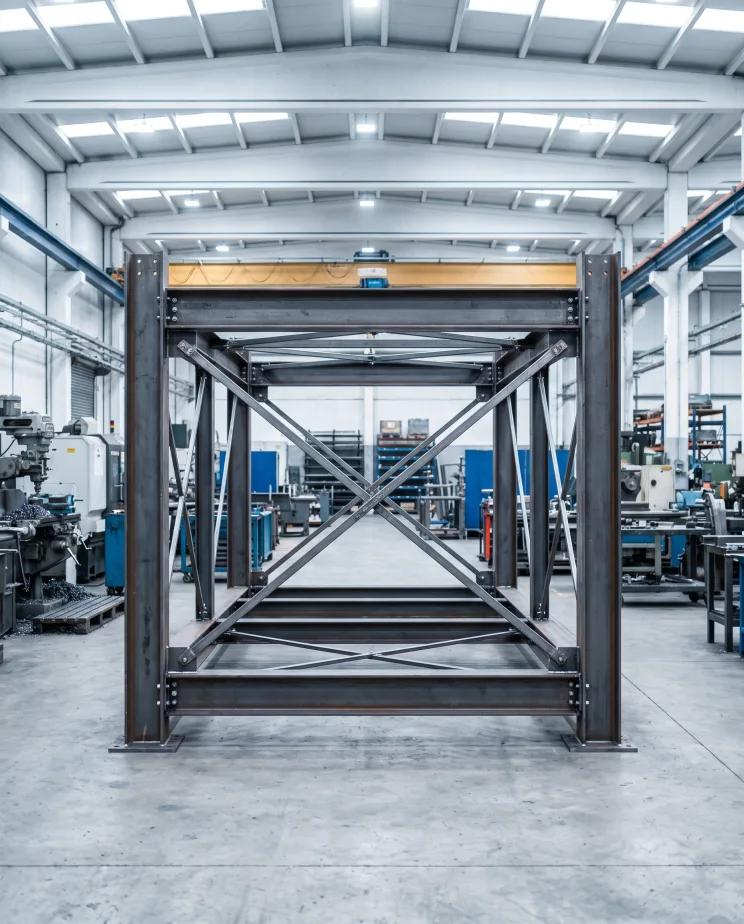
A fabricated steel frame assembled on a workshop floor with bolted connections and temporary bracing
Industrial steelwork — A fabricated steel frame, bolted and braced.
A stainless steel machine guard mounted on general industrial equipment
Machine guards and enclosures — A stainless guard on general equipment.
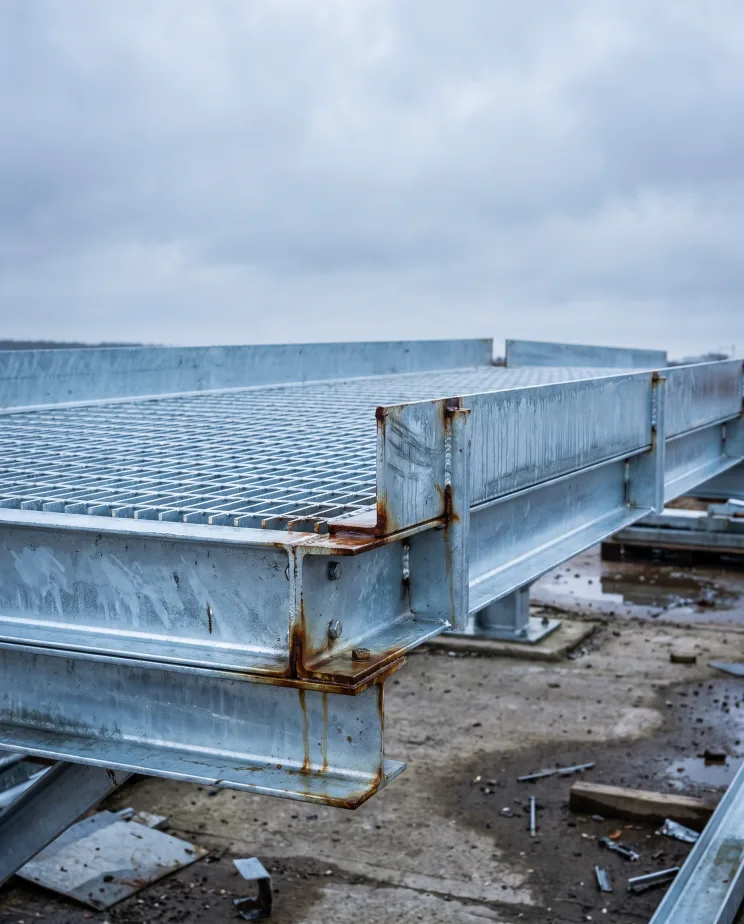
Galvanized steel grating and support brackets installed outdoors under an overcast sky
Outdoor and coastal parts — Galvanized grating and brackets, outdoors.

The company

Who does the work

Cold metal in, packed steel out — six processes under one roof.
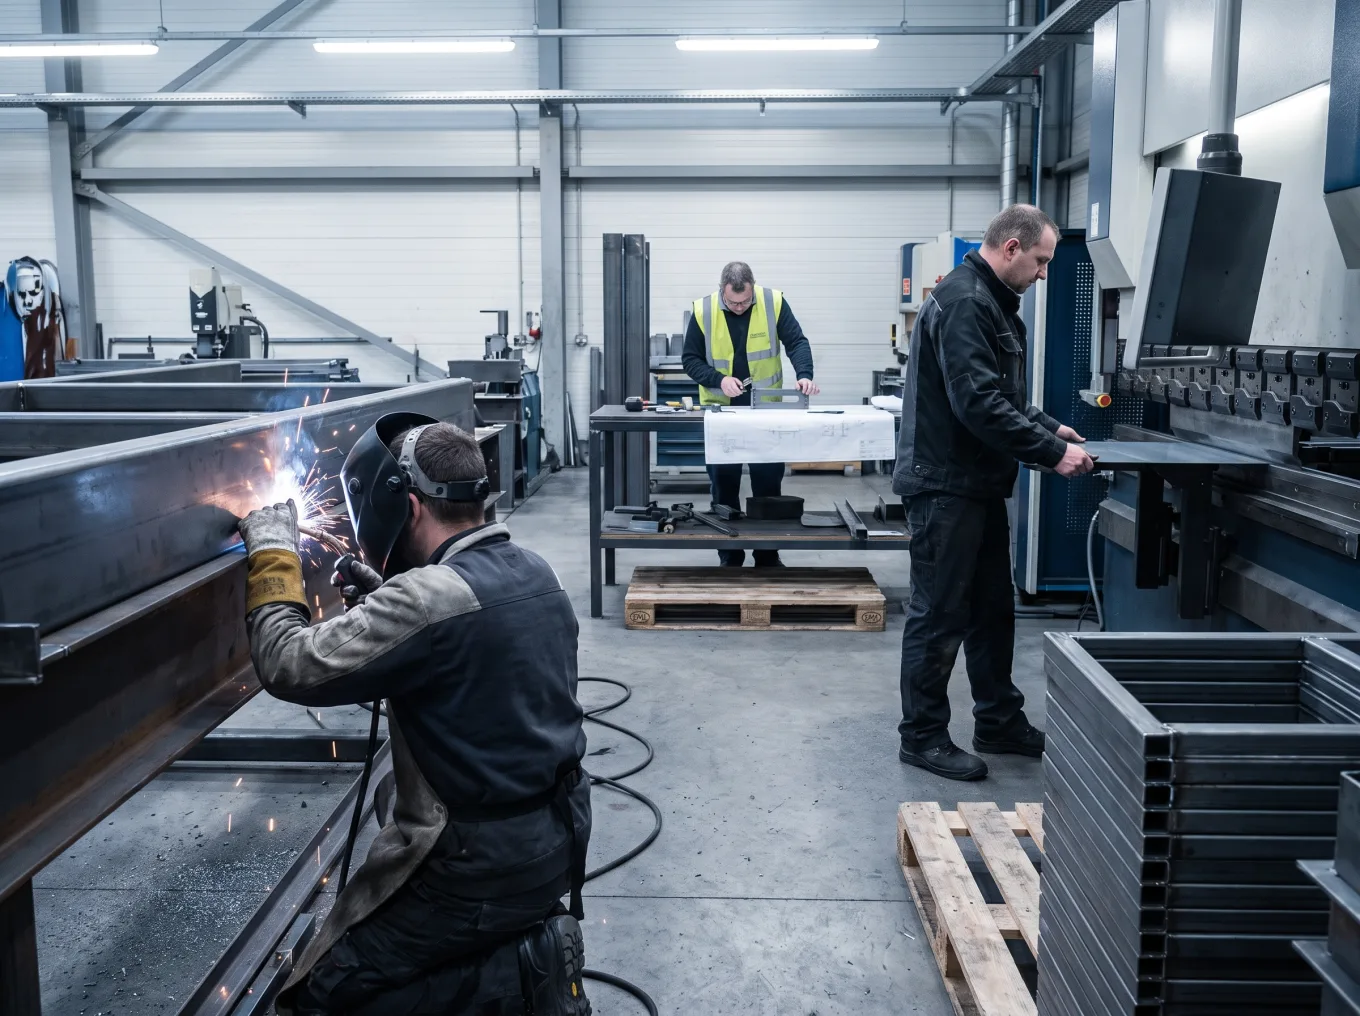
Welders, press-brake and inspection staff working at their own stations on the shop floor
Cutting, forming, welding, machining, finishing and inspection — the same crews on every job.
Founded
2004
Works area
42,000m²Covered bays and a galvanizing line
Export share
68%Shipped on FOB and CIF terms
Staff on site
246178 production · 24 QC · 18 engineering

Fibre laser cutting, press braking, welding with coded procedures, CNC machining, hot-dip galvanizing and a CMM room — all in house.

European Union
NL / DE / PL / ES
Australia and New Zealand
AU / NZ
Middle East
AE / SA / QA
North America
US / CA
Southeast Asia
ID / PH / MY / TH / VN

Published values are confirmed per project in the inspection plan issued with each order.
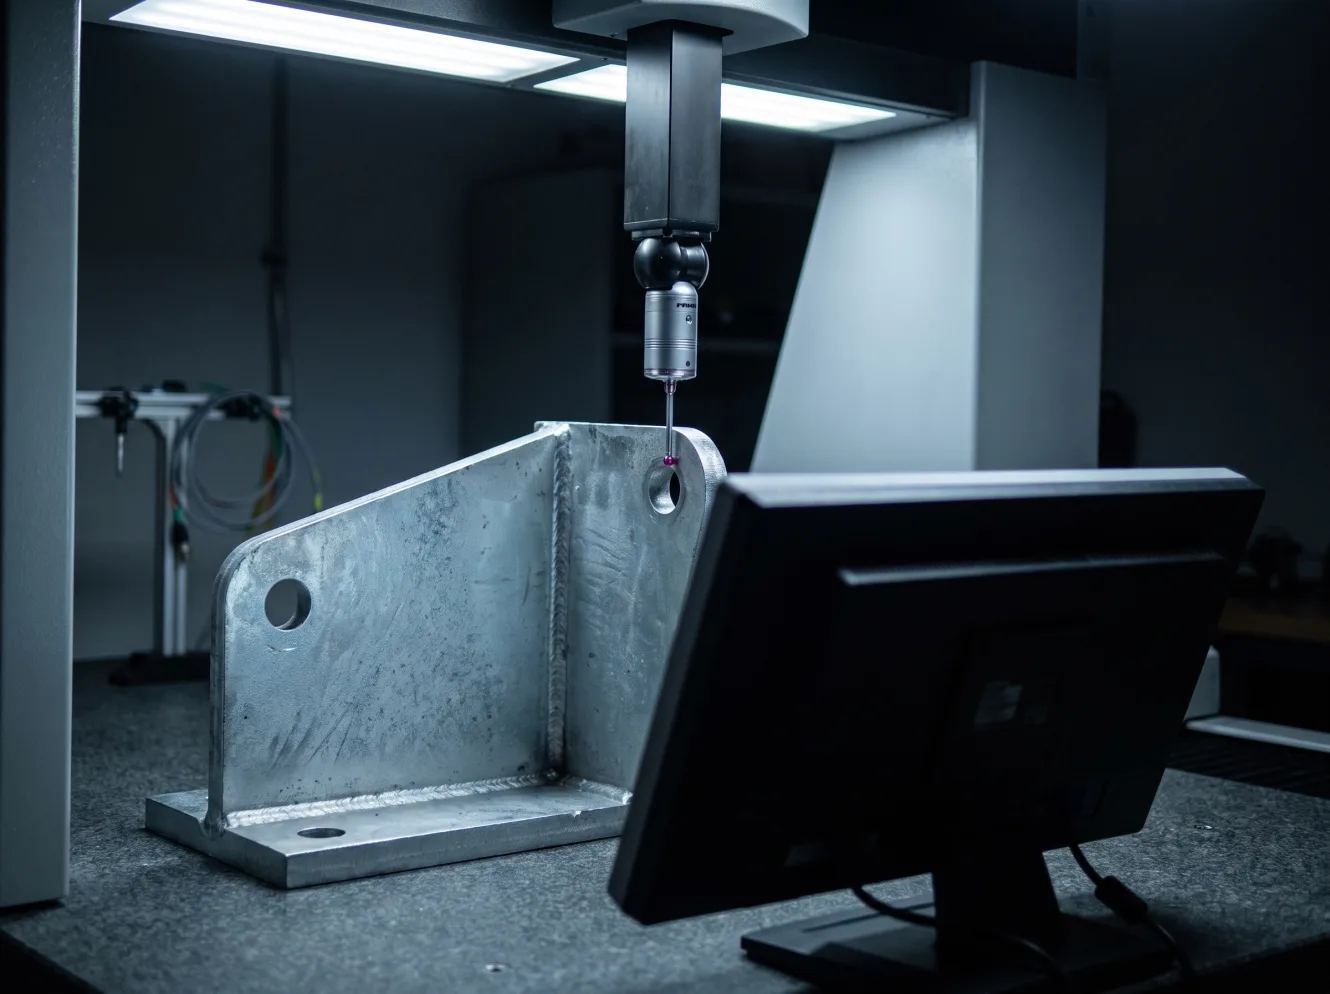
A coordinate measuring machine in a metrology room with its probe touching a hole in a galvanized steel bracket

Inside the plant

Every part measured before it ships

First article per drawing revision, sampling through the batch.
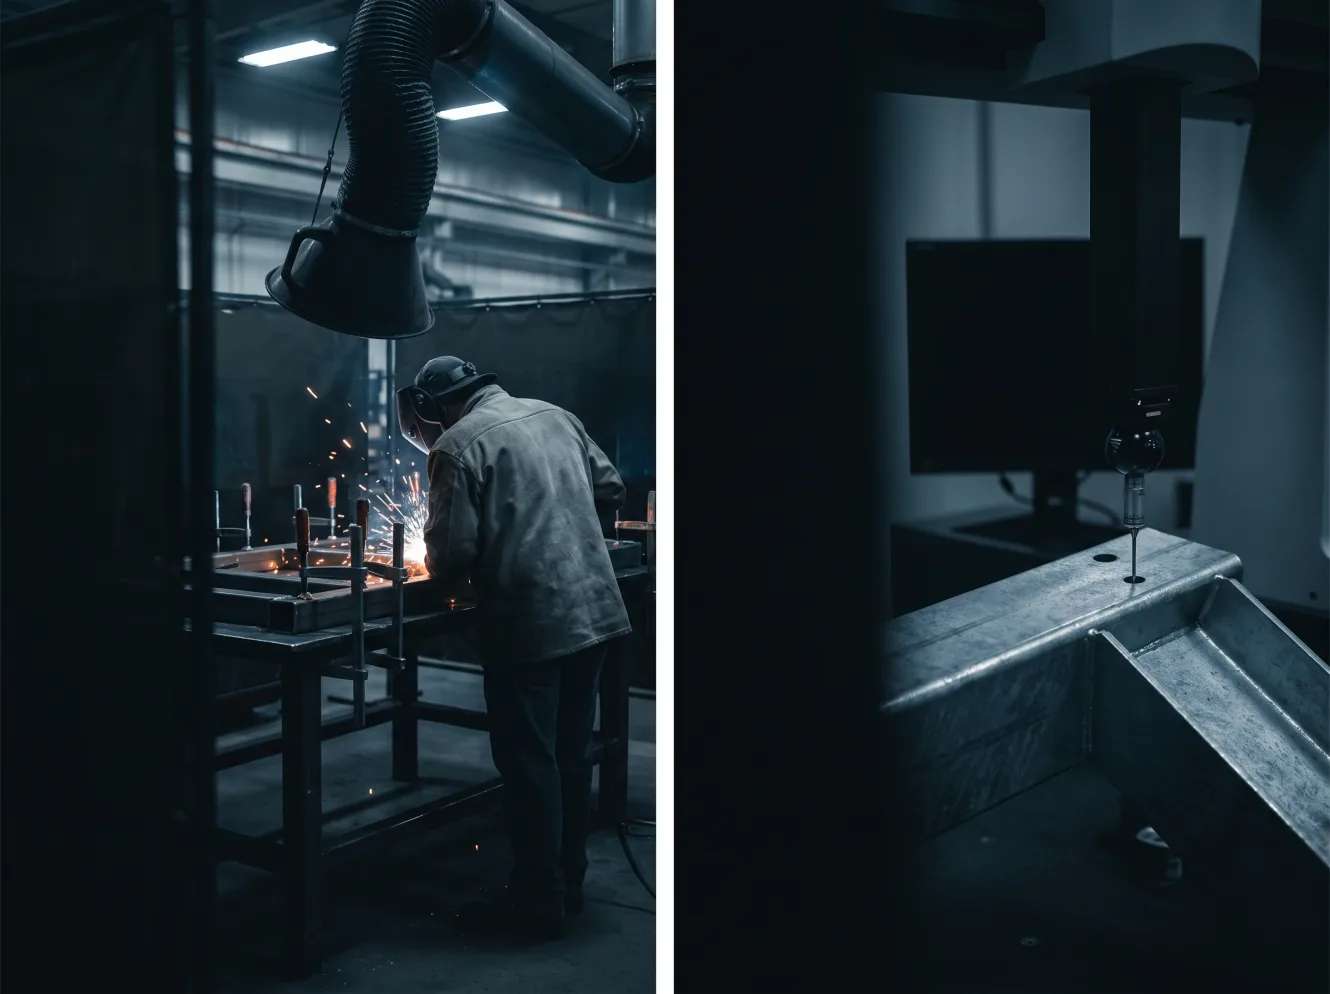
A welding bay on the shop floor with fume extraction ducting and fixture clamps, a welder working turned away from the camera
A coordinate measuring machine in a metrology room, its probe touching a hole in a galvanized steel bracket

Welding and QC

Welding and inspection

The two gates that decide whether a structural part is accepted: procedure and measurement.

Welding quality
ISO 3834-2full-scope quality requirements, procedures written per job
Procedure qualification
EN ISO 15614-1WPS issued and signed off before the first weld
Coded welders
96qualified to EN ISO 9606-1 and AWS D1.1
Non-destructive testing
100% / 10%visual on every weld, magnetic particle on 10% of structural runs
Dimensional check
CMMfirst article per drawing revision, plus sampling through the batch
Material traceability
EN 10204 3.1certificate with heat number, filed against the job number

Project values are confirmed in the inspection plan issued with each order.

Certification

Standards we build to

The six a compliance reviewer checks first. Numbers and issuing bodies follow with the quotation.
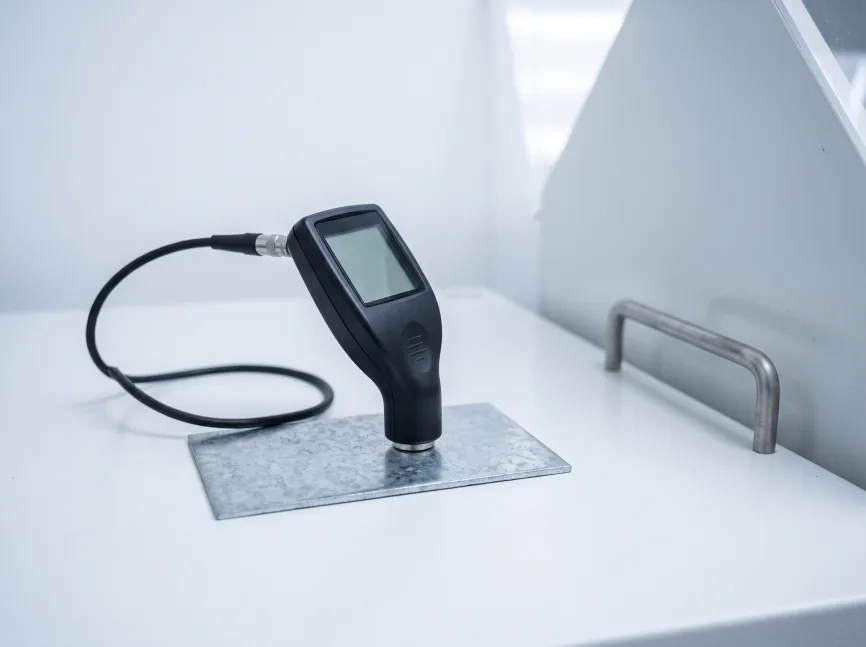
A coating thickness gauge with its probe pressed onto a galvanized steel plate on an inspection bench

EN 1090-2

Execution class EXC2, EXC3 on request

EU

ISO 3834-2

Welding quality requirements, full scope

EU / global

EN 10204 3.1

Material certificates, heat number traced

EU / global

ISO 1461

Hot-dip galvanizing, 85 µm minimum

EU / global

ISO 12944 C3–C5

Protective paint systems, 60–120 µm DFT

EU

ASTM B117

480 h neutral salt spray on coated parts

US / global

Enquiry

Send a drawing for quoting

Send the drawing, the standard and the quantity. We quote tolerance, certificates and a date.

  • Quotation turnaround2 working days on a complete drawing set
  • Sample lead time7–10 working days for one cut or machined part
  • DocumentsEN 10204 3.1, dimensional report, WPS, coating report
  • DrawingsDXF, DWG or STEP — attach the drawing set to the enquiry

sales@brantmoor.comWhatsApp

Drawings and confidentiality

Drawings, models and tolerances are held against the job number and released to nobody else.

We reply to every drawing enquiry within 24 hours on working days. Files are handled under the confidentiality terms in the quotation.